Same Drug, Different Attributes: Smarter Supply Planning for Global Expansion
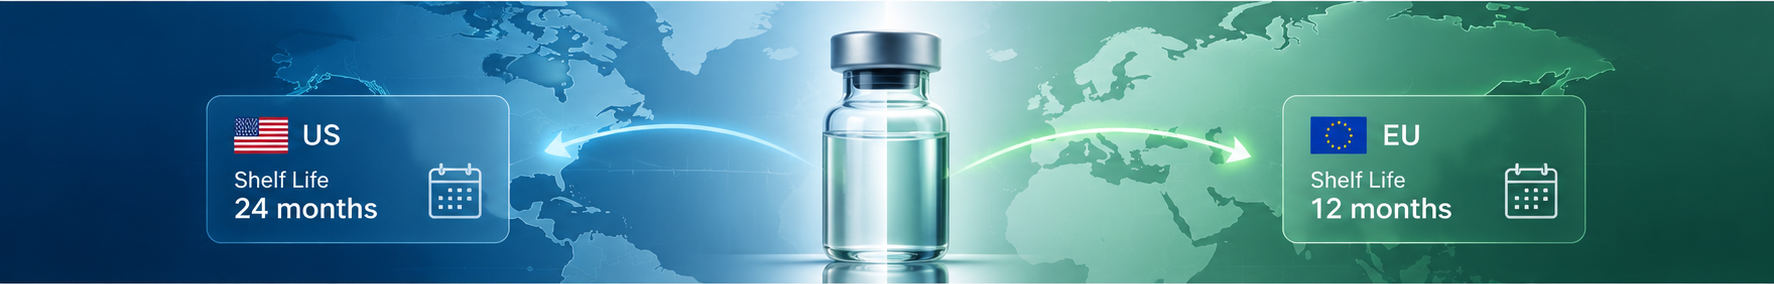
How a commercial-stage biotech company used ABC-Plan's flexible planning structure to manage regional shelf-life requirements while maintaining one integrated manufacturing plan.
The Challenge: One Product, Different Market Requirements
For a biotech company with an established commercial product in the United States, expanding into Europe represented an important next step in its growth.
However, as the company progressed through the regulatory review process in Europe and other EMEA markets, it became apparent that the approved shelf life could be shorter than what the FDA had granted for the US market.
This created an unexpected supply planning challenge.
The Drug Product (DP) was identical, regardless of whether it was destined for the US or European market. It came from the same manufacturing process and the same Contract Manufacturing Organization (CMO). Yet depending on its destination, the same material would need to be managed against different shelf-life requirements.
Traditional supply planning systems often rely on separate SKUs to distinguish between products with different planning characteristics. One possible approach would have been to create separate SKUs for the US and European markets.
But this didn't reflect how the company actually manufactured its product. The CMO was producing the same Drug Product, and introducing separate manufacturing SKUs solely to accommodate different regulatory shelf lives would add unnecessary complexity to production planning.
At the same time, treating all inventory as interchangeable without accounting for market-specific shelf-life requirements could result in poor allocation decisions, excess inventory, or unexpected shortages.
The supply chain team needed a way to manage different regional requirements while maintaining a common manufacturing plan.
The Solution: Different Shelf-Life Requirements, One Manufacturing SKU
ABC-Plan's flexible product structure allowed the supply chain team to address this challenge without creating separate manufacturing SKUs.
The planner configured different product "flavors" using separate planning nodes to represent the US and European markets. Each node could carry its own shelf-life requirements and safety stock targets, allowing inventory to be planned according to the specific needs of each market.
Manufacturing, however, continued to be planned at the SKU level. Since the Drug Product was identical regardless of its destination, the company could maintain one consolidated manufacturing plan for its CMO.
This separation was key. Market-specific requirements were managed at the planning-node level, while manufacturing remained at the common SKU level.
ABC-Plan's Master Planner could then optimize supply across the different planning nodes and material levels, taking into account demand, inventory requirements, and expiry risks without introducing unnecessary complexity into the manufacturing process.
Rather than forcing the company to create artificial SKUs or change how its CMO operated, ABC-Plan allowed the planning model to reflect the way the business actually worked.
Managing Expiry Risk Ahead of the European Launch
Shelf-life differences were only part of the challenge. With a new market launch approaching, the company also had to decide how much inventory to prepare before actual European demand became clear.
Producing too little could put the launch at risk. Producing too much could leave the company holding expensive inventory with a shorter usable shelf life than in the US.
ABC-Plan's expiry analysis provided an additional layer of visibility.
The team could evaluate inventory against market-specific shelf-life requirements, identify potential expiry exposure, and assess how different supply and demand assumptions might affect future inventory levels.
Combined with the Master Planner's optimization capabilities, this gave planners a way to evaluate the trade-offs between maintaining sufficient launch inventory and minimizing the risk of overstock.
Instead of relying on a single set of inventory assumptions across all markets, the company could make more informed decisions based on the requirements and uncertainties of each region.
The Outcome: One Integrated Supply Plan for Multiple Markets
By configuring market-specific product flavors within ABC-Plan, the company was able to address a complex planning requirement without introducing unnecessary changes to its manufacturing structure.
The resulting planning model allowed the team to:
· Maintain one manufacturing SKU while managing different regional shelf-life requirements.
· Plan safety stock independently for the US and European markets at the planning-node level.
· Generate optimized supply plans across multiple planning nodes and material levels.
· Evaluate inventory expiry risks as part of European launch preparations.
· Balance supply availability and excess inventory risks under different launch scenarios.
Perhaps the most valuable outcome was the ability to manage market-specific requirements without complicating the manufacturing process.
As the company prepared to enter new markets, its supply chain team gained greater visibility into potential supply and expiry risks while keeping production planning aligned with how the Drug Product was actually manufactured.
Looking Ahead: Planning for Growth Across Markets
International expansion often introduces supply planning challenges that go beyond increases in demand. Different regulatory approvals, shelf-life requirements, and market conditions can create significant differences in how the same product must be planned and managed.
For biotech companies relying on external manufacturing partners, these differences don't necessarily justify separate manufacturing SKUs or more complicated production processes.
ABC-Plan's flexible product structure and flavor (attribute-based) planning capabilities allow companies to account for regional requirements at the planning-node level while maintaining consolidated manufacturing plans at the SKU level.
In this case, the company was able to prepare for its European launch with a planning model that reflected both its manufacturing reality and market-specific requirements — without having to choose between the two.